
 Skip to content

In high-pressure hydrogen and hydrocarbon pipelines, the most critical external leakage point is often not a casting defect in the valve body, but the flange gasket. After repeated temperature cycling, flange bolts can experience stress relaxation, reducing gasket seating force. High-pressure hydrogen-containing hydrocarbons can then gradually escape through the gasket joint and, if exposed to an ignition source or static discharge, can ignite rapidly. Repeated combustible-gas alarms in process units are often traced to flange leakage.
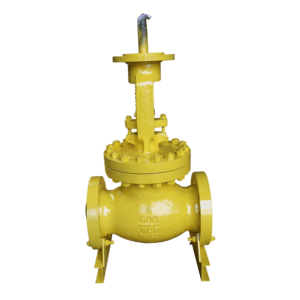
Butt weld check valves are welded directly to the pipeline at both ends. With no flanges, gaskets, or bolts, they eliminate this external leakage interface. The welded connection maintains its integrity under high pressure and is not subject to bolt relaxation and leakage after prolonged thermal cycling.
The bonnet uses a pressure-assisted self-sealing design. As process pressure increases, the metal sealing ring is pressed more tightly into position, improving sealing performance at higher pressures rather than developing the leakage risk associated with conventional gasketed bonnet connections.
For large-bore, high-pressure check valves, the disc incorporates a hydraulic cushioning mechanism. During closing, the disc is decelerated before contacting the seat, preventing severe impact from high-pressure reverse flow and water hammer. This protects the seat from deformation and reduces the risk of damage to the hinge pin and related components.
The sealing surfaces are hardfaced with Stellite 6 to resist erosion and surface degradation under prolonged exposure to high-pressure hydrogen-containing media, helping prevent internal leakage.
Butt-weld ends are machined strictly in accordance with ASME B16.25, allowing direct field welding without additional bevel modification.
Before shipment, every valve undergoes a high-pressure shell test at 1.5 times the design pressure, with test reports supplied with each valve.
Valve Design: Select a swing check valve for small-bore, high-velocity service; a lift check valve for vertical upward flow; and a large-bore swing check valve with hydraulic damping for pipelines with nominal diameters of DN300 and above.
Bonnet Sealing: For Class 900 and above, a pressure-assisted self-sealing bonnet is required. Conventional bolted gasketed bonnets are more susceptible to leakage after repeated high-temperature cycling.
Material Selection: For high-temperature hydrogen service, select F22 chromium-molybdenum alloy steel. For hydrogen sulfide service, select sour-service materials that comply with NACE MR0175 requirements.
Weld Ends: Before field welding, verify that the weld-end bevel dimensions comply with ASME B16.25 to prevent excessive mismatch, inadequate penetration, or unacceptable weld quality.
Q: How is a butt weld check valve serviced or repaired?
A: The valve uses a bolted bonnet and is fully serviceable. It can be cut out from the pipeline for workshop maintenance, or blind plates can be installed upstream and downstream before opening the bonnet for in-line maintenance. The valve is not permanently welded shut or non-removable.
Q: Can it be installed in a vertically upward-flowing pipeline?
A: Yes. A swing check valve can be used in horizontal pipelines and vertical upward-flow applications. For vertically downward flow, a spring-assisted closing design must be selected.
Q: What should be done if water hammer is severe under high-pressure service?
A: Large-bore, high-pressure versions can be equipped with a hydraulic damping cylinder. The disc closing speed can be controlled to reduce reverse-flow impact and prevent water hammer from damaging the valve body and sealing surfaces.
The recycle hydrogen and high-pressure water-injection pump discharge lines of a hydroprocessing unit operated by PetroChina Indonesia use NPS 3, Class 1500 check valves for high-temperature, high-pressure hydrogen-containing hydrocarbon service. The original flanged check valves experienced external leakage after gasket relaxation under cyclic thermal loading, repeatedly triggering combustible-gas alarms and forcing the unit to operate at reduced load.
Flowork supplied 48 NPS 2–6, Class 1500 butt weld check valves featuring A182 F22 chromium-molybdenum alloy steel bodies, pressure-assisted self-sealing bonnets, swing discs with hydraulic cushioning, Stellite 6 hardfaced sealing surfaces, and butt-weld ends machined in accordance with ASME B16.25. The valves were designed in accordance with API 594 and underwent shell and high-pressure seat leakage testing in accordance with API 598, with inspection witnessed on site by the PetroChina Indonesia inspection department.
Since entering service in October 2021, the valves have operated continuously for four years with zero external leakage. Combustible-gas alarm events have been reduced from five per year to zero, unplanned unit load reductions have fallen from four per year to zero, and hydroprocessing unit operating availability has increased to 98.7%.
Class150
Butt Weld Check Valve

| NPS | in | 2 | 2 1/2 | 3 | 4 | 5 | 6 | 8 | 10 | 12 | 14 | 16 | 18 | 20 | 24 |
| d | mm | 51 | 64 | 76 | 102 | 127 | 152 | 203 | 254 | 305 | 337 | 387 | 438 | 489 | 591 |
| L(RF) | mm | 203 | 216 | 241 | 292 | 330 | 356 | 495 | 622 | 699 | 787 | 864 | 978 | 978 | 1295 |
| L(BW) | mm | 203 | 216 | 241 | 292 | 330 | 356 | 495 | 622 | 699 | 787 | 864 | 978 | 978 | 1295 |
| L(RTJ) | mm | 216 | 229 | 254 | 305 | 343 | 368 | 508 | 635 | 711 | 800 | 876 | 991 | 991 | 1308 |
| d1 | mm | 92 | 105 | 127 | 157 | 186 | 216 | 270 | 324 | 381 | 413 | 470 | 533 | 584 | 692 |
| d2 | mm | 120.5 | 139.5 | 152.5 | 190.5 | 216 | 241.5 | 298.5 | 362 | 432 | 476 | 540 | 578 | 635 | 749.5 |
| D | mm | 152 | 178 | 190 | 229 | 254 | 279 | 343 | 406 | 483 | 533 | 597 | 635 | 699 | 813 |
| b | mm | 16 | 18 | 19 | 24 | 24 | 26 | 29 | 31 | 32 | 35 | 37 | 40 | 43 | 48 |
| n-Фd | mm | 4-19 | 4-19 | 4-19 | 8-19 | 8-22 | 8-22 | 8-22 | 12-25 | 12-25 | 12-29 | 16-29 | 16-32 | 20-32 | 20-35 |
| H | mm | 132 | 147 | 176 | 198 | 255 | 320 | 380 | 440 | 480 | 530 | 580 | 618 | 657 | 760 |
Class300
Butt Weld Check Valve

| NPS | in | 2 | 2 1/2 | 3 | 4 | 5 | 6 | 8 | 10 | 12 | 14 | 16 | 18 | 20 | 24 |
| d | mm | 51 | 64 | 76 | 102 | 127 | 152 | 203 | 254 | 305 | 337 | 387 | 432 | 483 | 584 |
| L(RF) | mm | 267 | 292 | 318 | 356 | 400 | 445 | 533 | 622 | 711 | 838 | 864 | 978 | 1016 | 1346 |
| L(BW) | mm | 267 | 292 | 318 | 356 | 400 | 445 | 533 | 622 | 711 | 838 | 864 | 978 | 1016 | 1346 |
| L(RTJ) | mm | 283 | 308 | 333 | 371 | 416 | 460 | 549 | 638 | 727 | 854 | 879 | 994 | 1035 | 1368 |
| d1 | mm | 92 | 105 | 127 | 157 | 186 | 216 | 270 | 324 | 381 | 413 | 470 | 533 | 584 | 692 |
| d2 | mm | 127 | 149 | 168.5 | 200 | 235 | 270 | 330 | 387.5 | 451 | 514.5 | 571.5 | 628.5 | 686 | 813 |
| D | mm | 165 | 190 | 210 | 254 | 279 | 318 | 381 | 445 | 521 | 584 | 648 | 711 | 775 | 914 |
| b | mm | 23 | 26 | 29 | 32 | 35 | 37 | 42 | 48 | 51 | 54 | 58 | 61 | 64 | 70 |
| n-Фd | mm | 8-19 | 8-22 | 8-22 | 8-22 | 8-22 | 12-22 | 12-25 | 16-29 | 16-32 | 20-32 | 20-35 | 24-35 | 24-35 | 24-41 |
| H | mm | 144 | 149 | 210 | 260 | 295 | 326 | 380 | 440 | 520 | 540 | 588 | 670 | 720 | 850 |
Class600
Butt Weld Check Valve

| NPS | in | 2 | 2 1/2 | 3 | 4 | 5 | 6 | 8 | 10 | 12 | 14 | 16 | 18 | 20 | 24 |
| d | mm | 51 | 64 | 76 | 102 | 127 | 152 | 200 | 248 | 298 | 327 | 375 | 419 | 464 | 559 |
| L(RF) | mm | 292 | 330 | 356 | 432 | 508 | 559 | 660 | 787 | 838 | 889 | 991 | 1092 | 1194 | 1397 |
| L(BW) | mm | 292 | 330 | 356 | 432 | 508 | 559 | 660 | 787 | 838 | 889 | 991 | 1092 | 1194 | 1397 |
| L(RTJ) | mm | 295 | 333 | 359 | 435 | 511 | 562 | 664 | 791 | 841 | 892 | 994 | 1095 | 1200 | 1407 |
| d1 | mm | 92 | 105 | 127 | 157 | 186 | 216 | 270 | 324 | 381 | 413 | 470 | 533 | 584 | 692 |
| d2 | mm | 127 | 149 | 168.5 | 216 | 267 | 292 | 349 | 432 | 489 | 527 | 603 | 654 | 724 | 838 |
| D | mm | 165 | 190 | 210 | 273 | 330 | 356 | 419 | 508 | 559 | 603 | 686 | 743 | 813 | 940 |
| b | mm | 26 | 29 | 32 | 38 | 45 | 48 | 56 | 64 | 67 | 70 | 77 | 83 | 89 | 102 |
| n-Фd | mm | 8-19 | 8-22 | 8-22 | 8-25 | 8-29 | 12-29 | 12-32 | 16-35 | 20-35 | 20-38 | 20-41 | 20-44 | 24-44 | 24-52 |
| H | mm | 170 | 178 | 246 | 290 | 320 | 360 | 430 | 502 | 554 | 595 | 680 | 778 | 970 | 1100 |
Class900
Butt Weld Check Valve

| NPS | in | 2 | 2 1/2 | 3 | 4 | 5 | 6 | 8 | 10 | 12 | 14 | 16 | 18 | 20 | 24 |
| d | mm | 47 | 57 | 73 | 98 | 121 | 146 | 190 | 234 | 282 | 311 | 354 | 400 | 444 | 533 |
| L(RF) | mm | 368 | 419 | 381 | 457 | 559 | 610 | 737 | 838 | 965 | 1029 | 1130 | 1219 | 1321 | 1549 |
| L(BW) | mm | 368 | 419 | 381 | 457 | 559 | 610 | 737 | 838 | 965 | 1029 | 1130 | 1219 | 1321 | 1549 |
| L(RTJ) | mm | 371 | 422 | 384 | 460 | 562 | 613 | 740 | 841 | 968 | 1038 | 1140 | 1232 | 1334 | 1568 |
| d1 | mm | 92 | 105 | 127 | 157 | 186 | 216 | 270 | 324 | 381 | 413 | 470 | 533 | 584 | 692 |
| d2 | mm | 165 | 190.5 | 190.5 | 235 | 279.4 | 317.5 | 393.7 | 469.9 | 533.4 | 558.8 | 615.9 | 685.8 | 749.3 | 901.7 |
| D | mm | 216 | 244 | 241 | 292 | 349 | 381 | 470 | 545 | 610 | 640 | 705 | 785 | 855 | 1040 |
| b | mm | 38.5 | 41.5 | 38.5 | 44.5 | 51 | 56 | 64 | 70 | 79.5 | 86 | 89 | 102 | 108 | 140 |
| n-Фd | mm | 8-26 | 8-29 | 8-26 | 8-32 | 8-35 | 12-32 | 12-39 | 16-39 | 20-39 | 20-42 | 20-45 | 20-51 | 20-54 | 20-67 |
| H | mm | 200 | 220 | 280 | 320 | 360 | 400 | 480 | 560 | 630 | 680 | 780 | 880 | 1050 | 1200 |
Class1500
Butt Weld Check Valve

| NPS | in | 2 | 2 1/2 | 3 | 4 | 5 | 6 | 8 | 10 | 12 | 14 | 16 |
| d | mm | 47 | 57 | 70 | 92 | 111 | 136 | 178 | 222 | 263 | 289 | 330 |
| L(RF) | mm | 368 | 419 | 470 | 546 | 673 | 705 | 832 | 991 | 1130 | 1257 | 1384 |
| L(BW) | mm | 368 | 419 | 470 | 546 | 673 | 705 | 832 | 991 | 1130 | 1257 | 1384 |
| L(RTJ) | mm | 371 | 422 | 473 | 549 | 676 | 711 | 841 | 1000 | 1146 | 1276 | 1407 |
| d1 | mm | 92 | 105 | 127 | 157 | 186 | 216 | 270 | 324 | 381 | 413 | 470 |
| d2 | mm | 165 | 190.5 | 203.2 | 241.3 | 292.1 | 317.5 | 393.7 | 482.6 | 571.5 | 635 | 704.8 |
| D | mm | 216 | 244 | 267 | 311 | 375 | 394 | 483 | 585 | 675 | 750 | 825 |
| b | mm | 38.5 | 41.5 | 48 | 54 | 73.5 | 83 | 92.9 | 108 | 124 | 133.5 | 146.5 |
| n-Фd | mm | 8-26 | 8-29 | 8-32 | 8-35 | 8-42 | 12-39 | 12-45 | 12-51 | 16-54 | 16-61 | 16-67 |
| H | mm | 210 | 240 | 303 | 340 | 380 | 430 | 500 | 590 | 660 | 710 | 820 |
Class2500
Butt Weld Check Valve

| NPS | in | 2 | 2 1/2 | 3 | 4 | 5 | 6 | 8 | 10 | 12 |
| d | mm | 38 | 47 | 57 | 73 | 92 | 111 | 146 | 184 | 219 |
| L(RF) | mm | 451 | 508 | 578 | 673 | 794 | 914 | 1022 | 1270 | 1422 |
| L(BW) | mm | 451 | 508 | 578 | 673 | 794 | 914 | 1022 | 1270 | 1422 |
| L(RTJ) | mm | 454 | 514 | 584 | 683 | 807 | 927 | 1038 | 1292 | 1445 |
| d1 | mm | 92 | 105 | 127 | 157 | 186 | 216 | 270 | 324 | 381 |
| d2 | mm | 171.4 | 196.8 | 228.6 | 273 | 323.8 | 368.3 | 438.1 | 539.7 | 619.1 |
| D | mm | 235 | 267 | 305 | 356 | 419 | 483 | 550 | 675 | 760 |
| b | mm | 51 | 57.5 | 67 | 76.5 | 92.5 | 108 | 127 | 165.5 | 184.5 |
| n-Фd | mm | 8-29 | 8-32 | 8-35 | 8-42 | 8-48 | 8-54 | 12-54 | 12-67 | 12-74 |
| H | mm | 230 | 260 | 330 | 370 | 410 | 460 | 530 | 620 | 690 |
API Trim NO.
Table
|
No |
Seat |
Gate、disc 、ball or body |
Stem |
No |
Seat |
Gate、disc 、ball or body |
Stem | |
| 01 | 13Cr | 13Cr | 13Cr | 31 | STELLITE | 321SS | 321SS | |
| 02 | 304SS | 304SS | 304SS | 32 | STELLITE | STELLITE | 321SS | |
| 03 | 310SS | 310SS | 310SS | 33 | 347SS | 347SS | 347SS | |
| 04 | HARD 13Cr | HARD 13Cr | 13Cr | 34 | STELLITE | 347SS | 347SS | |
| 05 | STELLITE | STELLITE | 13Cr | 35 | NICKEL ALLOY | 13Cr | 13Cr | |
| 06 | Cu-Ni | 13Cr | 13Cr | 36 | A105/PTFE | A105+ENP | A105+ENP | |
| 07 | 13Cr | HARD 13Cr | 13Cr | 37 | A105/PTFE | WCB+ENP | A105+ENP | |
| 08 | STELLITE | 13Cr | 13Cr | 38 | 13Cr/PTFE | 13Cr | 13Cr | |
| 09 | Cu-Ni | Cu-Ni | Cu-Ni | 39 | 304SS/PTFE | 304SS | 304SS | |
| 10 | 316SS | 316SS | 316SS | 40 | 316SS/PTFE | 316SS | 316SS | |
| 11 | Cu-Ni | STELLITE | Cu-Ni | 41 | A105/RPTFE | A105+ENP | A105+ENP | |
| 12 | STELLITE | 316SS | 316SS | 42 | A105/RPTFE | WCB+ENP | A105+ENP | |
| 13 | ALLOY 20 | ALLOY 20 | ALLOY 20 | 43 | 13Cr/RPTFE | 13Cr | 13Cr | |
| 14 | STELLITE | ALLOY 20 | ALLOY 20 | 44 | 304SS/RPTFE | 304SS | 304SS | |
| 15 | STELLITE | STELLITE | 304SS | 45 | 316SS/RPTFE | 316SS | 316SS | |
| 16 | STELLITE | STELLITE | 316SS | 46 | A105/NYLON | A105+ENP | A105+ENP | |
| 17 | STELLITE | STELLITE | 347SS | 47 | A105/NYLON | WCB+ENP | A105+ENP | |
| 18 | STELLITE | STELLITE | ALLOY 20 | 48 | A105/NYLON | 304SS | 304SS | |
| 19 | MONEL | MONEL | MONEL | 49 | A105/NYLON | 316SS | 316SS | |
| 20 | BRONZE | BRONZE | 13Cr | 50 | 13Cr/NYLON | 13Cr | 13Cr | |
| 21 | HASTELLOY B | HASTELLOY B | HASTELLOY B | 51 | 304SS/NYLON | 304SS | 304SS | |
| 22 |
| HASTELLOY C | HASTELLOY C | 52 | 316SS/NYLON | 316SS | 316SS | |
| 23 | STELLITE | 304SS | 304SS | 53 | A105/PEEK | A105+ENP | A105+ENP | |
| 24 | 304LSS | 304LSS | 304LSS | 54 | A105/PEEK | WCB+ENP | A105+ENP | |
| 25 | STELLITE | 304LSS | 304LSS | 55 | 13Cr/PEEK | 13Cr | 13Cr | |
| 26 | STELLITE | STELLITE | 304LSS | 56 | 304SS/PEEK | 304SS | 304SS | |
| 27 | 316LSS | 316LSS | 316LSS | 57 | 316SS/PEEK | 316SS | 316SS | |
| 28 | STELLITE | 316LSS | 316LSS |
|
|
|
|
|
| 29 | STELLITE | STELLITE | 316LSS |
|
|
| ||
| 30 | 321SS | 321SS | 321SS |
|
|
|
| |
Note:please indicate it directly in the
order for the internal part’smaterial uncovered in the table


 Optimized by Seraphinite Accelerator